Hardness Control for Sour-Service Fasteners (B7M / L7M / 2HM): NACE MR0175 / ISO 15156 Practical Guide
Why Hardness Is the Control Point for Sour-Service Fasteners
A fastener that passes tensile, yield, and dimensional checks can still fail in service in a sour well. When carbon or low-alloy steel is exposed to wet H2S, hydrogen atoms diffuse into the steel and can initiate sulfide stress cracking (SSC) — a brittle failure that occurs at loads far below yield. The susceptibility of a steel to SSC increases with its hardness. Above a threshold hardness, even a correctly torqued stud can crack within weeks of service.
NACE MR0175 / ISO 15156-2 is the internationally accepted materials standard for this environment. For carbon and low-alloy steels used as bolts, studs, nuts, and washers in sour service, it sets a maximum hardness of 22 HRC on the finished part. This 22 HRC maximum is the non-negotiable upper limit for SSC prevention in sour service. While mechanical tensile and yield strength remain critical for structural integrity, exceeding 22 HRC disqualifies the fastener for wet H2S environments, regardless of its theoretical tensile capacity.
The practical implication for buyers: hardness is not merely a routine MTC test item — it is a primary compliance gatekeeper. And because it is easy to test incorrectly, hardness verification is also one of the most common sources of rejected fastener shipments in MENA EPC projects. For the full compliance framework around these grades, start with our comprehensive NACE MR0175 / ISO 15156 compliance overview.
Where the 22 HRC Limit Comes From — and Which Scale Is Used for Acceptance
The hardness cap is defined in NACE MR0175 / ISO 15156-2 for carbon and low-alloy steels used in H2S-containing environments (Table A.1 in the applicable edition of the standard). The requirements apply to the finished fastener, not the raw material:
| Material group | Maximum hardness (NACE) | Product-standard control range | Typical grades |
|---|---|---|---|
| Carbon & low-alloy steel (sour service) | 22 HRC | ASTM A193 B7M: 200–235 HBW (93–99 HRB); A320 L7M: 200–235 HBW (93–99 HRB); A194 2HM: 159–237 HBW (84–99 HRB) | B7M, L7M, 2HM |
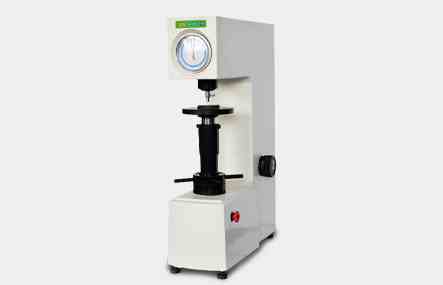
Which scale do labs and MTCs actually use? NACE MR0175 states the limit as 22 HRC, but 22 HRC sits at the extreme low end of the Rockwell C scale, where measurement uncertainty is largest. For this reason, the ASTM product standards control the M-grades in HBW or HRB: ASTM A193 (B7M), A320 (L7M), and A194 (2HM) specify hardness acceptance in HBW/HRB, and this is what appears as the primary hardness data on EN 10204 MTCs. ISO 15156-2 also states that hardness values shall be reported in the scale used for testing, and conversion between scales shall not be used for acceptance purposes unless specifically permitted by the purchasing specification. In practice, MENA EPCs (Aramco, ADNOC, PDO) reject MTCs that report converted values without stating the original test scale. Always state the test method and scale, and report raw readings — conversions (per ASTM E140) are a cross-check, not the acceptance value.
The lower bound matters too. B7M and L7M are specified at 200–235 HBW (93–99 HRB), and 2HM at 159–237 HBW (84–99 HRB). Over-tempering produces a fastener soft enough to pass the upper limit but too weak to meet the tensile and yield requirements of the product standard. A lot that is "soft enough" on the hardness report can still be rejected on mechanical testing — and is a real risk in sour service where strength and hardness must both hold.
M-grade vs standard grades:
| Grade | Standard | Sour service | Hardness control | Notes |
|---|---|---|---|---|
| B7 | ASTM A193 | Usually not specified | 28–34 HRC typical | Strength grade; above the 22 HRC cap |
| B7M | ASTM A193 | Yes | 200–235 HBW (93–99 HRB); ≤ 22 HRC | Tempered for sour service; 100% hardness testing required |
| L7 | ASTM A320 | Usually not specified | Higher hardness | Low-temperature grade |
| L7M | ASTM A320 | Yes | 200–235 HBW (93–99 HRB); ≤ 22 HRC | Low-temperature + sour service |
| 2H | ASTM A194 | Not for sour service | Higher hardness | Standard nut grade |
| 2HM | ASTM A194 | Yes | 159–237 HBW (84–99 HRB); ≤ 22 HRC | Sour-service nut grade |
Why M-grades exist: the standard B7 and L7 grades are supplied at a higher hardness for strength (typically 28–34 HRC), which places them above the sour-service limit. B7M, L7M, and 2HM are the same alloy systems processed and tempered to a controlled, lower hardness — staying below 22 HRC while retaining adequate mechanical strength.
Tempering requirements: B7M and L7M require a minimum tempering temperature of 620 °C (1150 °F); the 2HM nut grade requires a minimum of 650 °C (1200 °F). These are mandatory processing requirements in the ASTM standards. If the heat-treatment chart shows tempering below the minimum, the lot fails the material specification directly — a non-conformance event — regardless of whether the final hardness readings happen to meet 22 HRC. Insufficient tempering leaves high residual stress and an unstable microstructure, which is precisely the condition that promotes SSC.
When a project specification calls for "NACE-compliant" stud bolts, it is calling for these M-grades, and the hardness record is the proof.
Choosing the Right Hardness Test Method
Three hardness scales dominate fastener inspection, and each has a role:
Vickers / micro-Vickers (ISO 6507, ASTM E384)
- Small indentation, high precision, works on curved surfaces and narrow zones.
- Thread roots and thin sections must be tested with micro-Vickers (HV0.3, HV0.5, or at most HV1) — a HV10 indentation (diagonal ≈ 0.25–0.30 mm) is too large for a standard thread-root radius and produces edge effects that invalidate the reading. Measure below the root surface (e.g., 0.1–0.15 mm beneath the flank) on a sectioned sample.
- HV10 remains acceptable for larger, flat cross-sections of the shank or body where geometry permits.
Rockwell C (ASTM E18 / ISO 6508, HRC scale)
- Fast, standard, and widely understood; the scale named in the NACE 22 HRC limit.
- Suitable for flat, adequately sized surfaces such as a bolt head face or a nut face.
- Not suitable for thin sections, thread roots, or small-diameter fasteners; and at the low end of the scale (around 22 HRC) measurement uncertainty increases, which is why product standards prefer HBW/HRB for acceptance.
Brinell (ASTM E10 / ISO 6506, HBW)
- Large indentation averages the material over a bigger area; good for larger sections.
- Commonly reported as HBW 10/3000 or 10/500 — the primary acceptance scale for B7M/L7M/2HM.
Method selection rule of thumb: use Brinell (HBW) or Rockwell (HRB/HRC) on flat head and nut faces for acceptance data; use micro-Vickers (HV0.3–HV1) on thread roots and thin sections. Report the method, the load, and the test location for every reading — a hardness value without a method and location is not verifiable.
Testing the Full Cross-Section — and the 100% Production Check
Two different hardness controls apply to sour-service fasteners, and it is important not to confuse them:
- 100% non-destructive hardness testing (production check): ASTM A193 requires Grade B7M to be hardness-tested on every full-size fastener (typically on the end face or shank surface), unlike standard B7 which is sampled per lot. This is the manufacturer's mandatory outgoing check.
- Destructive cross-sectional mapping (sampling per heat-treat lot): a small number of samples per lot are sectioned and mapped across head, shank, and thread root to verify the full cross-section (base material and, where applicable, any weld-affected zone — welding is rare on standard fasteners but relevant on custom fabricated items). This is what an EN 10204 3.2 third-party inspection will typically witness.
For a machined or cold-formed fastener, the practical hotspots in cross-sectional mapping are:
- Thread roots — the thread rolling or cutting process can work-harden or decarburize the root, changing local hardness. A part that measures 20 HRC on the head can show a different value at the thread root. Test roots with micro-Vickers on a sectioned sample.
- Reduced shank and grip sections — any machined diameter change is a potential stress concentrator; verify hardness there.
- Head-to-shank transition — cold heading or forging can locally harden this fillet.
Thread-rolling sequence is a decisive manufacturing detail. If threads are roll-formed after quench-and-temper heat treatment, the thread root work-hardens severely — root hardness can climb to 28–30 HRC and scrap the lot at third-party micro-hardness sampling. B7M/L7M bolts should be rolled before final heat treatment, or given a full stress-relief anneal after rolling, so the root stays below the 22 HRC / 250 HV threshold.
Practical tip from our inspection team: when sectioning a sample for hardness mapping, we mark the cut plane on the drawing before testing. This avoids confusion between "3rd thread from the end" and "5th thread from the end" when the inspector is reviewing the report months later. A 30-second marking step prevents a 3-day document hold.
Marking Test Locations on the Report
A hardness test result is only as good as its traceability. Each reading in the report should be tied to a specific location on the part, typically by:
- a schematic drawing of the fastener with numbered test points;
- a coordinate description (e.g., "thread root, 3rd full thread from the end, HV0.5 = 241");
- the part identity and heat/lot number.
When the report shows five readings but no indication of where they were taken, an EPC QA/QC engineer should treat it as an incomplete submission. This is a leading cause of document-hold at receiving inspection, and it is fully preventable on the supplier side.
Common Hardness Rejection Scenarios in Sour-Service Orders
| Scenario | What goes wrong | How to prevent it |
|---|---|---|
| Head-only testing | Certificate reports head hardness only; thread roots unverified | Section a sample per lot; test thread roots with micro-Vickers |
| Wrong scale | Values converted without stating the original scale; HRC used near its measurement floor | Report raw readings in HBW/HRB per the product standard |
| Over-limit readings | One reading above 22 HRC (e.g., 24–26 HRC on a work-hardened thread root) | Confirm the thread-rolling sequence and tempering schedule; re-process before shipment |
| Under-limit readings | Over-tempered lot below the HBW minimum — tensile/yield will fail | Verify the lower bound (200 HBW for B7M/L7M; 159 HBW for 2HM), not just the upper limit |
| Coating interference | Hardness taken over a zinc or PTFE coating, giving false readings | Test on uncoated areas or after stripping the coating locally |
| Batch gaps | Only one sample tested for a large lot; no per-heat coverage | Define sampling per the project inspection plan; cover each heat represented in the lot |
| MTC mismatch | MTC hardness values do not match the delivered batch's markings | Tie every test record to heat number and lot marking; reconcile before packing |
Field experience note: in our work supplying L7M studs for offshore sour-gas projects in the Arabian Gulf, the most frequent rejection trigger is not base-metal hardness — it is thread-root readings after roll threading done post-heat-treatment. Localized work hardening can push thread-root values to 24–26 HRC if the rolling sequence is wrong or stress relief is skipped. We now specify roll-before-heat-treatment (or a stress-relief anneal after rolling) and thread-root micro-Vickers testing as standard for all sour-service orders, not just when the customer specifies it.
How Hardness Records Fit Into the EN 10204 MTC Package
For MENA oil and gas procurement, hardness is reported inside the material inspection certificate. A compliant submission typically contains:
- EN 10204 3.1 or 3.2 MTC — material grade, heat number, chemical composition, mechanical properties (tensile, yield, elongation), and hardness results;
- Hardness test report — scale, load, test locations, individual readings, and the acceptance limits applied (22 HRC maximum; HBW/HRB ranges per product standard);
- Heat-treatment records — time-and-temperature furnace charts demonstrating minimum tempering temperatures (620 °C for B7M/L7M; 650 °C for 2HM);
- Traceability chain — heat number on MTC ↔ wire rod batch ↔ production lot ↔ package marking ↔ head marking on the fastener.
The head marking matters: each B7M or L7M stud should carry the grade, manufacturer mark, and a short heat code. QA/QC engineers should be able to pick any box, read the head marking, and find that exact heat in the MTC with matching hardness values. If the chain breaks anywhere, the lot is rejected even if the steel is physically fine. For the field-side verification workflow, see our practical audit procedures for sour-service fasteners.
Acceptance Checklist for QA/QC Engineers at Receiving Inspection
- Confirm the project specification calls for NACE MR0175 / ISO 15156-2 compliance and identifies the applicable requirements.
- Verify the grades are M-grades (B7M, L7M, 2HM, or equivalent) — not standard B7/L7/2H.
- Check the MTC is EN 10204 3.1 or 3.2 as specified, with a unique heat number.
- Confirm hardness values are within the product-standard ranges (B7M/L7M: 200–235 HBW or 93–99 HRB; 2HM: 159–237 HBW or 84–99 HRB), in the original test scale.
- Verify test method and load are stated (HBW 10/3000, HRB, HRC, micro-Vickers HV0.3–HV1, etc.).
- Confirm test locations cover base material and thread roots, not only the head.
- Confirm the heat-treatment chart shows tempering ≥ 620 °C (B7M/L7M) or ≥ 650 °C (2HM).
- Match head markings to the MTC heat numbers on a random sample of boxes.
- If the MTC shows values near the limits, request additional samples for independent verification.
- Where the contract requires 3.2, confirm the third-party inspector's signature and stamp are present.
- Keep the hardness report and MTC together in the project dossier for audit traceability.
Frequently Asked Questions
What happens if fastener hardness exceeds 22 HRC in sour service?
The part becomes susceptible to sulfide stress cracking in wet H2S service. Even a single reading above the limit on a critical location (for example a work-hardened thread root) is grounds for rejection of that lot under NACE MR0175 / ISO 15156-2.
Can I substitute B7 for B7M if hardness is below 22 HRC?
Not reliably. Standard B7 is not processed with controlled tempering, full-section verification, or the mandatory 100% hardness testing that applies to B7M. Specify the M-grade for sour service and verify the heat-treatment chart, not just the final reading.
Why do MTCs report HBW/HRB instead of HRC if the limit is 22 HRC?
Because 22 HRC sits at the extreme low end of the Rockwell C scale, where measurement uncertainty is largest. The ASTM product standards (A193, A320, A194) therefore control the M-grades in HBW/HRB, and ISO 15156-2 requires hardness to be reported in the scale used for testing. HRC is the conceptual NACE limit; HBW/HRB are the acceptance data on the certificate.
Which hardness test should be used on thread roots?
Micro-Vickers per ASTM E384 / ISO 6507, typically HV0.3, HV0.5, or at most HV1, measured just below the root surface on a sectioned sample. Standard HV10 indentations are too large for thread-root radii.
Do nuts need the same hardness control as bolts?
Yes. Nuts in sour service (e.g., A194 2HM) are controlled at 159–237 HBW (84–99 HRB) and are subject to the same 22 HRC maximum under NACE MR0175 / ISO 15156-2.
What is the sampling requirement for hardness testing per NACE MR0175?
Follow the project inspection plan, purchase order, or agreed inspection plan. A common starting point is a minimum of two parts per heat and at least three locations per part, with sectioning for thread-root verification. Note that B7M additionally requires 100% non-destructive hardness testing of full-size fasteners per ASTM A193. For critical sour-service orders, EPCs often request EN 10204 3.2 third-party witness testing.
Does a zinc or PTFE coating affect hardness testing?
Yes. Coatings change the measured value. Test on uncoated areas, on a prepared flat spot, or on a sectioned sample after local coating removal.
Take the Next Step on Your Sour-Service Fastener Order
Get hardness control wrong, and a fastener that looks perfect on paper will fail in the field. If you are specifying B7M / L7M stud bolts or 2HM nuts for a sour project, send us your BOM and the applicable project specification. We will confirm the M-grade processing, the heat-treatment route, the thread-rolling sequence, and the hardness test plan (locations, methods, and sample sizes), and return a sample EN 10204 3.1 package with full hardness data for your QA/QC team to review — typically within 24 hours.
Why work with us on sour-service fasteners:
- We supply NACE MR0175 / ISO 15156-compliant fasteners to EPC contractors across the MENA region, including projects for national oil companies in Saudi Arabia, the UAE, and Qatar.
- Our quality system is certified to ISO 9001:2015, and we work with accredited third-party inspectors (TÜV, BV, SGS) for EN 10204 3.2 certification.
- For sour-service orders, we provide a complete document package: EN 10204 3.1/3.2 MTC, hardness test reports with location mapping, heat-treatment charts, and full traceability from wire rod to finished fastener.
Typical response timeline:
- Technical review and sample MTC package: 24 hours for standard grades (B7M, L7M, 2HM)
- Commercial quotation: 48 hours for standard items, 72 hours for custom or exotic alloys
- Sample production: 2–3 weeks depending on grade and quantity
Next steps:
- Need a technical reference for your internal review? Ask for our sour-service fastener hardness checklist (PDF).
- Need sample parts for validation? Request B7M / 2HM sample sets with head markings for your inspection team.
- Need a project quotation? Send the drawing or standard with quantities and delivery dates for a reviewed commercial offer.
- Need pre-production QA review? Send your PO and specification before ordering, and we will provide a review of the inspection plan and document requirements at no charge.